Changing tube size involves more than loading a new cutting length. Before the next product enters the cutoff, the project should confirm its dimensional requirements, cutting arrangement, clamping setup and operating conditions.
For an ERW tube mill line, these checks should form part of the overall size-change procedure. A completed forming-roll change does not, by itself, confirm that the cutoff is ready for the next product.
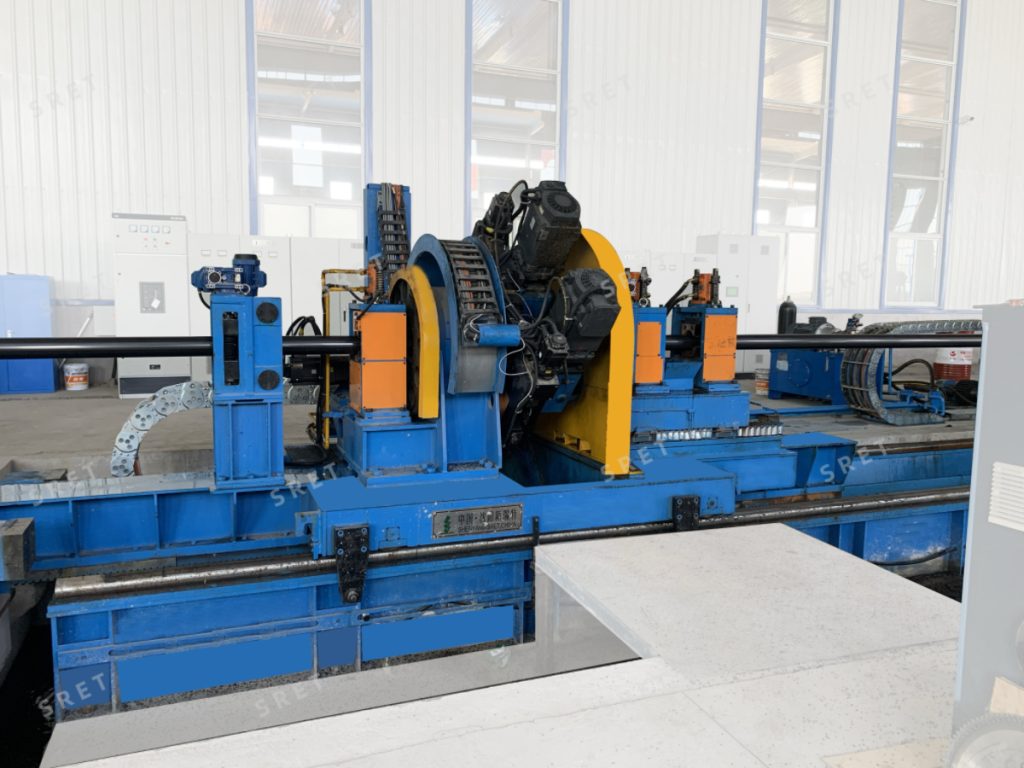
This guide focuses on the information and checks needed for that transition. For equipment descriptions, feeding-path options and published model specifications, see SRET’s orbital milling type flying cutoff.
A tube size alone is not a complete cutting specification.
Before reviewing a changeover, identify the tube profile, dimensions, wall thickness, material specification, required cut length and intended line speed.
The required cut-end condition and length acceptance should also be documented.
| Product Item | Information to Confirm |
| Profile | Round, square or rectangular |
| Dimensions | Diameter or section width and height |
| Wall thickness | Applicable thickness for the production order |
| Material | Grade and relevant material condition |
| Cut length | Required finished length |
| Operating speed | Intended production condition |
| Acceptance | Length and cut-end inspection requirements |
For rectangular tubes, state width and height separately. A model table listing round and square dimensions should not be interpreted as confirming every rectangular combination.
Where the product falls outside the published information, request application confirmation rather than infer suitability from a similar section.
A published maximum speed does not establish the operating speed available for every tube and cut length.
The cutoff must complete its required movements within the available production cycle. The review should therefore consider the intended cut length and line speed together with the product being cut.
Ask the supplier to confirm the proposed operating condition, including:
Do not assume that maximum section size, maximum wall thickness, shortest cut length and maximum speed can all be combined.
When the cutoff serves an existing tube mill line, use the actual production schedule as the basis for this review—not only the highest speed shown in an equipment table.
SRET’s product page describes polar-coordinate and rectangular-coordinate profiling feeding paths. It also separately introduces a high-speed dual-mode version capable of selecting between single-blade sawing and double-blade milling.
These descriptions should not be treated as interchangeable configurations.
Before a product change, establish:
The purpose is not to reselect the machine at every changeover. It is to ensure that the next product is covered by the installed configuration and approved setup.
Do not assume that a feature described for one version is available on every orbital milling cutoff.
The changeover procedure should identify the tube’s position relative to the cutting system.
Confirm the applicable mill reference, the cutoff setup requirements and the support arrangement for the next section.
SRET describes reduced saw-height adjustment requirements for its rectangular-coordinate arrangement. The project documentation should state how that feature applies to the supplied machine and the intended product range.
Useful questions include:
For a tube mill machine with a fixed-bottom-line forming arrangement, make that design basis explicit. It should not remain an assumption shared informally between different equipment teams.
Clamping requirements should be reviewed separately from the cutting program.
The changeover documentation should identify which jaws and support settings apply to each approved product or product group.
Record:
SRET’s product page describes reduced clamp-jaw requirements for its rectangular-coordinate design. Treat that as a configuration-specific feature, not a promise that one jaw arrangement suits every tube size and profile.
The practical objective is a clear setup instruction. Operators should not need to infer the correct jaw arrangement from a general product brochure.
A change in tube size does not automatically mean that the existing blade and cutting settings remain appropriate.
The project should identify the approved blade specification and cutting program for the intended product.
SRET’s product page lists TCT or HSS blade options. That does not mean the two are interchangeable without reviewing the application.
Confirm the applicable requirements for:
Where stored programs are included in the supplied control system, establish how the correct program is selected and verified.
Do not add a promise of automatic recipe selection or parameter retention unless that function has been confirmed for the machine.
An upstream roller change and a cutoff setup change are related activities, but they are not the same task.
The line-changeover plan should identify who confirms readiness at the sizing section, cutoff and receiving equipment.
The agreed sequence should address:
Avoid assuming that a roller quick-change system automatically updates the cutoff.
If data exchange or coordinated setup functions are included, describe the actual interface and its responsibilities in the project documentation.
The changeover procedure should define how the initial cut product is checked.
Use the agreed acceptance requirements rather than relying only on a general description such as “smooth cutting.”
The inspection plan may address:
The measurement method, acceptance limits and person responsible for release should be established in advance.
If downstream end facing or hydrostatic testing is required, retain the relevant requirements for those operations. A satisfactory cutoff inspection should not be presented as a guarantee that every later inspection will pass.
All setup and trial activities should follow the supplied operating and machinery-safety procedures.
A concise changeover record can connect the approved product with its required setup.
| Record Item | Information to Retain |
| Product identification | Profile, dimensions, thickness and material |
| Production condition | Cut length and approved operating speed |
| Cutting arrangement | Feeding path and applicable cutting mode |
| Mechanical setup | Jaws, supports and relevant reference settings |
| Blade | Approved specification and condition check |
| Program | Applicable program or setup reference |
| Inspection | First-off results and release approval |
| Exceptions | Outstanding limitations or additional checks |
Keep proposed settings separate from approved production settings.
Where the same nominal tube size is produced in different materials or wall thicknesses, confirm whether separate setup records are required.
A reliable orbital milling cutoff changeover starts with a defined product and an approved operating condition.
The review should connect tube dimensions, cut length, speed, reference position, clamping and cutting setup. First-off inspection then provides the agreed basis for releasing the next production batch.
This approach keeps the changeover discussion focused on the supplied machine and the actual production requirement, rather than assuming that every configuration shares the same adjustments or automatic functions.