Automatic tube stacking is only one part of preparing finished tubes for storage and dispatch. Before selecting a handling arrangement, the project should define what the completed stack must look like and how it will move into the next packaging operation.
Questions about layer patterns, tube-end alignment and strapping responsibilities are best resolved before the equipment layout is finalized. They turn a general request for automated handling into a clearer production requirement.
For an ERW tube mill line, these planning decisions should clarify how cut tubes enter the stacking area and how completed stacks are handed over for strapping. This guide focuses on those planning decisions. For available stacking mechanisms, automation arrangements and packaging-line scope, see SRET’s automatic tube packaging machine.
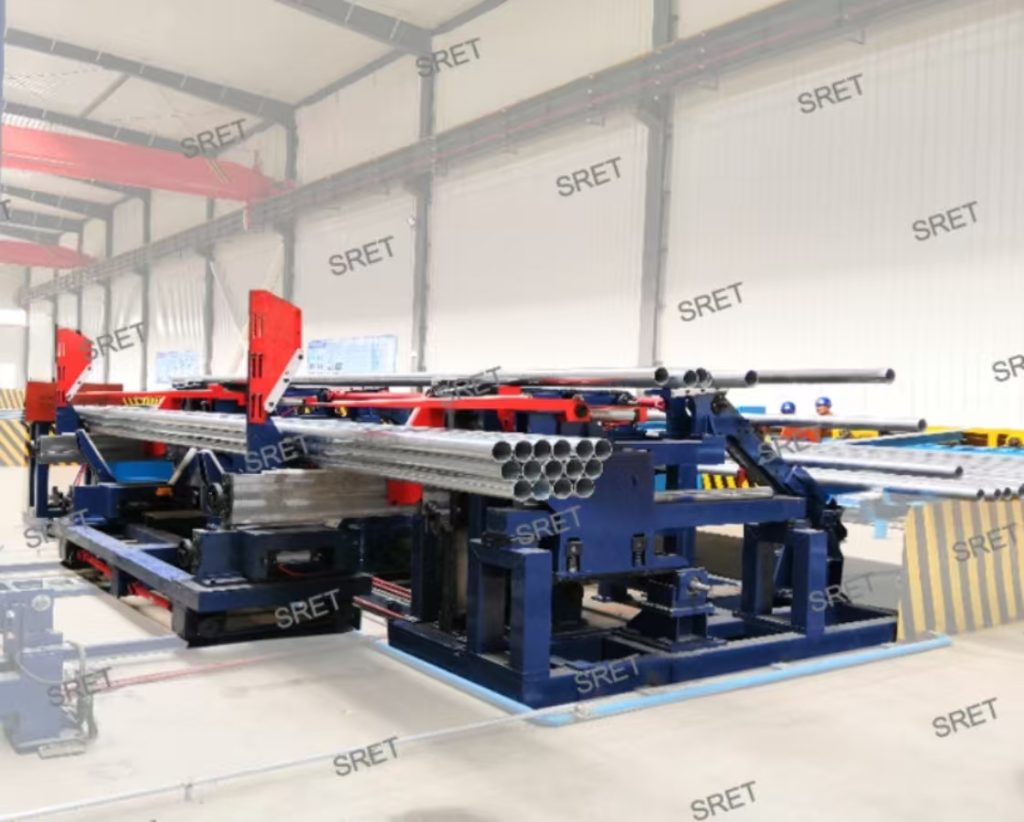
The shape of an individual tube and the shape of a finished bundle are different specifications.
Round, square and rectangular describe the tube profile. Square, rectangular and hexagonal can describe the arrangement of the completed bundle. A packaging proposal should identify both rather than use “shape” as a single, undefined requirement.
A useful starting specification includes:
For example, stating that the line handles round tubes does not explain whether the required output is a rectangular or hexagonal bundle. The intended bundle arrangement must be defined separately.
It should also be clear whether a production batch contains one tube length or requires another agreed handling arrangement. Do not assume that mixed lengths are included simply because the equipment can handle several product sizes.
“Layer-by-layer stacking” describes a method, but it does not fully define the required output.
The project should establish how many tubes form each layer, how many layers complete the stack and whether successive layers use the same arrangement.
Document the following:
| Planning Item | Requirement to Define |
| Tubes per layer | Target quantity and any permitted variation |
| Number of layers | Required completed-stack arrangement |
| Layer sequence | Repeated or alternating pattern, where applicable |
| Stack completion | Whether completion is determined by count, weight or another agreed condition |
| Incomplete layer | What should happen at the end of a batch |
| Product change | How remaining tubes from the previous batch are handled |
An incomplete layer deserves particular attention. If a batch ends before the planned quantity is reached, the required operator action and handling procedure should be agreed rather than left undefined.
The specification should also distinguish the intended pattern from the means of producing it. A required layer arrangement does not automatically confirm a particular adjustment method or control feature.
A bundle requirement should explain which tube ends must align and what reference is used.
For a batch of nominally equal-length tubes, the project may specify alignment at one end. If another arrangement is required, it should be shown in the layout or acceptance documentation.
Questions to resolve include:
These requirements should be coordinated with the incoming cut-tube condition. Packaging specifications should not silently assume that downstream alignment will compensate for every upstream length or transfer issue.
Avoid describing the result only as “neat stacking.” A defined reference and an agreed acceptance condition make the requirement easier to communicate and verify.
The original production flow may include receiving, water removal, counting, conveying, alignment and stacking. However, the final sequence should reflect the equipment actually included in the project.
If a water-blowing unit is required, identify its position, responsibilities and acceptance conditions. It should not be presented as a standard part of every packaging configuration unless that scope has been confirmed.
Surface requirements also need a practical definition. State the relevant tube finish, the permitted contact conditions and the inspection method to be used during acceptance.
For handling evaluation, provide representative product information rather than relying only on a general statement such as “scratch-free operation.”
Where surface protection is important, ask the supplier to review the proposed contact and transfer arrangement against the actual tube specification. Any claimed result should be tied to the agreed product and operating conditions.
Completing a stack and securing a bundle are separate stages.
SRET’s packaging-line scope allows fully automatic or semi-automatic arrangements. Therefore, a project description should state whether strapping is performed manually or by an integrated automatic strapping machine.
The handover requirement should explain:
The number and positions of straps should also be confirmed for the intended product and bundle length. They should not be treated as universal settings for every application.
If manual strapping is selected, describe the line as automatic stacking with manual strapping rather than calling the complete packaging process fully automatic.
Access, guarding and operating procedures for that arrangement must be reviewed through the project’s machinery-safety process. This planning guide does not replace the supplied safety instructions.
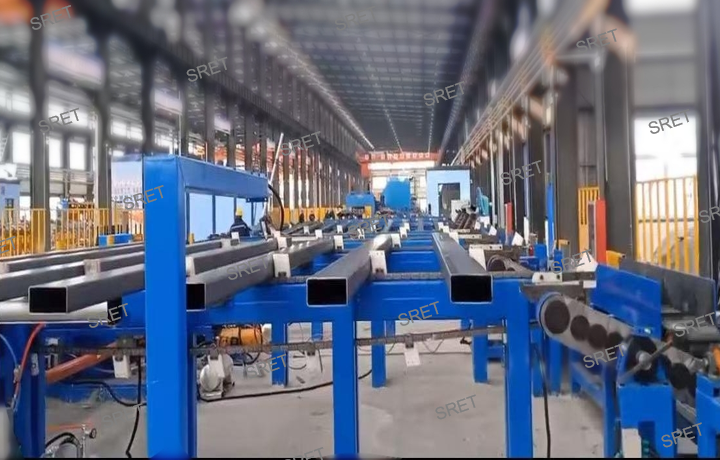
The packaging layout should show the agreed destination of the secured bundle.
Depending on the supply scope, subsequent operations may include transfer, weighing, labeling or movement toward a final storage area. Identify which of these belong to the packaging line and which are handled by separate equipment or the customer’s personnel.
Useful interface questions include:
These questions are particularly important when the stacking section and downstream equipment are supplied under different contracts.
A process-flow arrow should represent an agreed transfer responsibility, not simply imply that two neighboring machines will work together automatically.
A product range is not a complete changeover description.
For each planned change in tube dimensions, length or bundle arrangement, identify which settings need to change and how the change is performed.
Separate the following categories:
This avoids interpreting “adjustable” as meaning that every setting changes automatically.
For fork-arm stacking in particular, confirm the applicable adjustment range and the method supplied for the project. Where a magnetic handling arrangement is proposed, have the supplier confirm compatibility with the intended products and operating conditions.
The article’s purpose is not to declare one mechanism universally better. It is to make the required result and adjustment responsibilities clear before equipment selection.
A short requirements sheet can bring these decisions together before the packaging-line proposal is finalized.
| Category | Information to Provide |
| Tube specification | Profile, dimensions, length, weight and relevant surface condition |
| Production batches | Product consistency and planned changeover conditions |
| Bundle arrangement | Cross-section, tubes per layer and layer sequence |
| Completion rule | Required quantity, weight or other agreed condition |
| End alignment | Reference end and acceptance requirement |
| Incoming preparation | Any required water removal or other included operation |
| Strapping | Manual or automatic, with agreed strap arrangement |
| Downstream handling | Transfer destination and receiving responsibility |
| Control interfaces | Required permissions, status signals and interruption handling |
| Acceptance | Test products, demonstrated functions and inspection records |
Use this sheet to distinguish a requested capability from a confirmed supply item.
A proposed layout should then show how each agreed requirement is addressed, including any items outside the equipment supplier’s scope.
Effective tube stacking planning starts with a defined output: the required bundle shape, layer arrangement, end alignment and handover condition.
Once these requirements are clear, the project can evaluate the appropriate handling mechanism and automation scope without confusing automatic stacking with complete packaging automation.
The finished specification should connect the incoming tube condition with the required secured bundle and its next destination. That gives equipment selection, layout review and acceptance testing a shared basis.