A shear end welder combines strip-end preparation and joining, but completing an automatic cycle is only one part of commissioning. The project must also establish whether the supplied equipment handles the agreed strip specifications, produces an acceptable joint and returns the entry section to a condition ready for feeding.
For an ERW tube mill line, these checks should be agreed before the equipment enters production. They provide a clearer acceptance basis than general statements such as “high welding quality” or “easy operation.”
This article focuses on commissioning scope and acceptance requirements. For machine descriptions, published strip ranges and model-specific welding options, see SRET’s shear end welder product page.
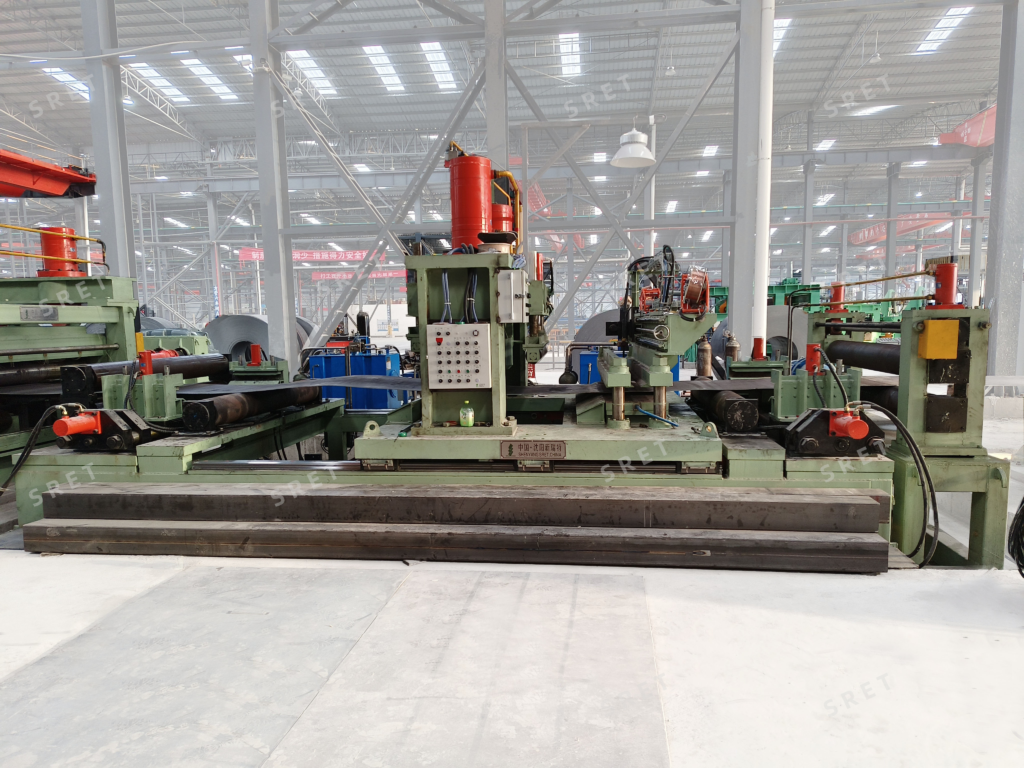
A commissioning plan should identify the strip used for demonstration.
Record the material grade, width and thickness, together with the applicable preparation and welding requirements. Where the proposed production range includes several materials or significantly different dimensions, agree on which conditions will be demonstrated and which require additional review.
The test plan should distinguish between:
These checks answer different questions. Demonstrating machine movement does not, by itself, confirm suitability for every material within the published dimensional range.
For an ERW tube mill project, the acceptance conditions should reflect the intended strip application rather than the finished-tube diameter alone.
The equipment sequence includes both strip centering and longitudinal positioning. Commissioning should verify their respective functions rather than combine them into one general alignment check.
The review should establish how the outgoing tail and incoming head are located relative to the machine reference. It should also confirm how each end reaches the required trimming position.
Record which adjustments are powered, which are automatic and which require operator confirmation.
Useful questions include:
This creates a documented basis for operation and troubleshooting.
The joining result should not be assessed only after welding.
The acceptance procedure should include a check of the trimmed ends and the required joint arrangement. The applicable end condition, positioning requirements and joint gap should follow the approved setup for the selected material and welding process.
Do not apply one universal gap or trimming requirement to every machine and application.
When reviewing a tube mill machine installation, confirm how the equipment establishes the welding position after shearing. Also identify the clamps that retain the prepared ends during welding.
The temporary overlap used during the published preparation sequence should not be mistaken for the final joint type. The subsequent joining operation establishes a butt-joint arrangement.
The term “automatic shear end welder” does not identify one welding process.
SRET’s published model table lists TIG, TIG/MIG and MIG configurations across the range. The technical documentation should state the process supplied for the selected equipment and the conditions under which it will be demonstrated.
Depending on that process, confirm the applicable requirements for:
For an ERW tube mill machine proposal, avoid treating features from one welding configuration as standard across the entire range.
A visual demonstration of automatic welding is not a complete quality-acceptance method.
Before commissioning, agree on how the joint will be inspected and what constitutes an acceptable result. The requirements should identify the applicable inspection procedure, acceptance criteria and responsibility for approval.
The project should also establish how rejected joints are handled. This includes the permitted recovery procedure and the conditions required before strip transfer resumes.
Where downstream passage is part of the acceptance scope, identify the equipment and operating conditions involved. Do not assume that a successful welding cycle alone proves every requirement of the complete production line.
The product table lists model-specific cycle times. For project acceptance, the timing boundary should be explicit.
A cycle-time review should identify its starting and finishing events. It should also state whether the quoted figure includes operator actions, material presentation, inspection and any additional handling.
| Timing Item | Point to Confirm |
| Start condition | What must be ready before timing begins |
| Included actions | Which preparation and welding movements are counted |
| Operator tasks | Whether required manual actions are included |
| Inspection | Whether joint checks fall inside or outside the figure |
| Finish condition | Whether timing ends after welding, reset or feeding readiness |
Use the same definitions when comparing the proposal with the commissioning result.
The overall interruption in entry feeding can then be reviewed separately against the accumulator’s available reserve and the intended tube mill line operating conditions.
The shear end welder operates between upstream strip preparation and downstream storage. Commissioning should therefore include the agreed interfaces, not only the machine’s internal movements.
Check the signals and conditions required to receive strip, begin preparation and resume transfer. Confirm which equipment controls each action and where operator authorization is required.
The review should also address interrupted cycles and abnormal conditions. The operating documentation should explain the approved response to a positioning problem, unsuccessful weld or other interruption.
Recovery should follow the supplied instructions and machine-safety requirements. A commissioning article is not a substitute for those procedures.
The commissioning record should connect the demonstrated functions with the agreed supply scope.
Useful handover information includes:
This documentation helps distinguish a demonstrated capability from a general product claim.
A useful commissioning plan examines material suitability, positioning, end preparation, welding, inspection and line interfaces as separate acceptance items.
The objective is not simply to show that the machine can move automatically. It is to confirm the functions included in the contract under defined operating conditions.
For published model capacities, cycle times and welding options, refer to SRET’s shear end welder specifications. Project-specific acceptance requirements should then be agreed in the technical proposal.